Bag thickness is a useful buying specification, but it cannot diagnose every leaking or difficult-to-seal pack. Punctures, contamination, folds, material construction and unsuitable machine settings may produce similar failures. Start with the actual product and process, then choose a gauge that works within that complete system.
A thicker film may help an otherwise comparable pouch resist some handling damage. That does not mean every thicker bag is stronger than every thinner one, or that a particular micron value makes exposed bones harmless. Use a representative sample trial to confirm the finished pack.
Microns and Mils
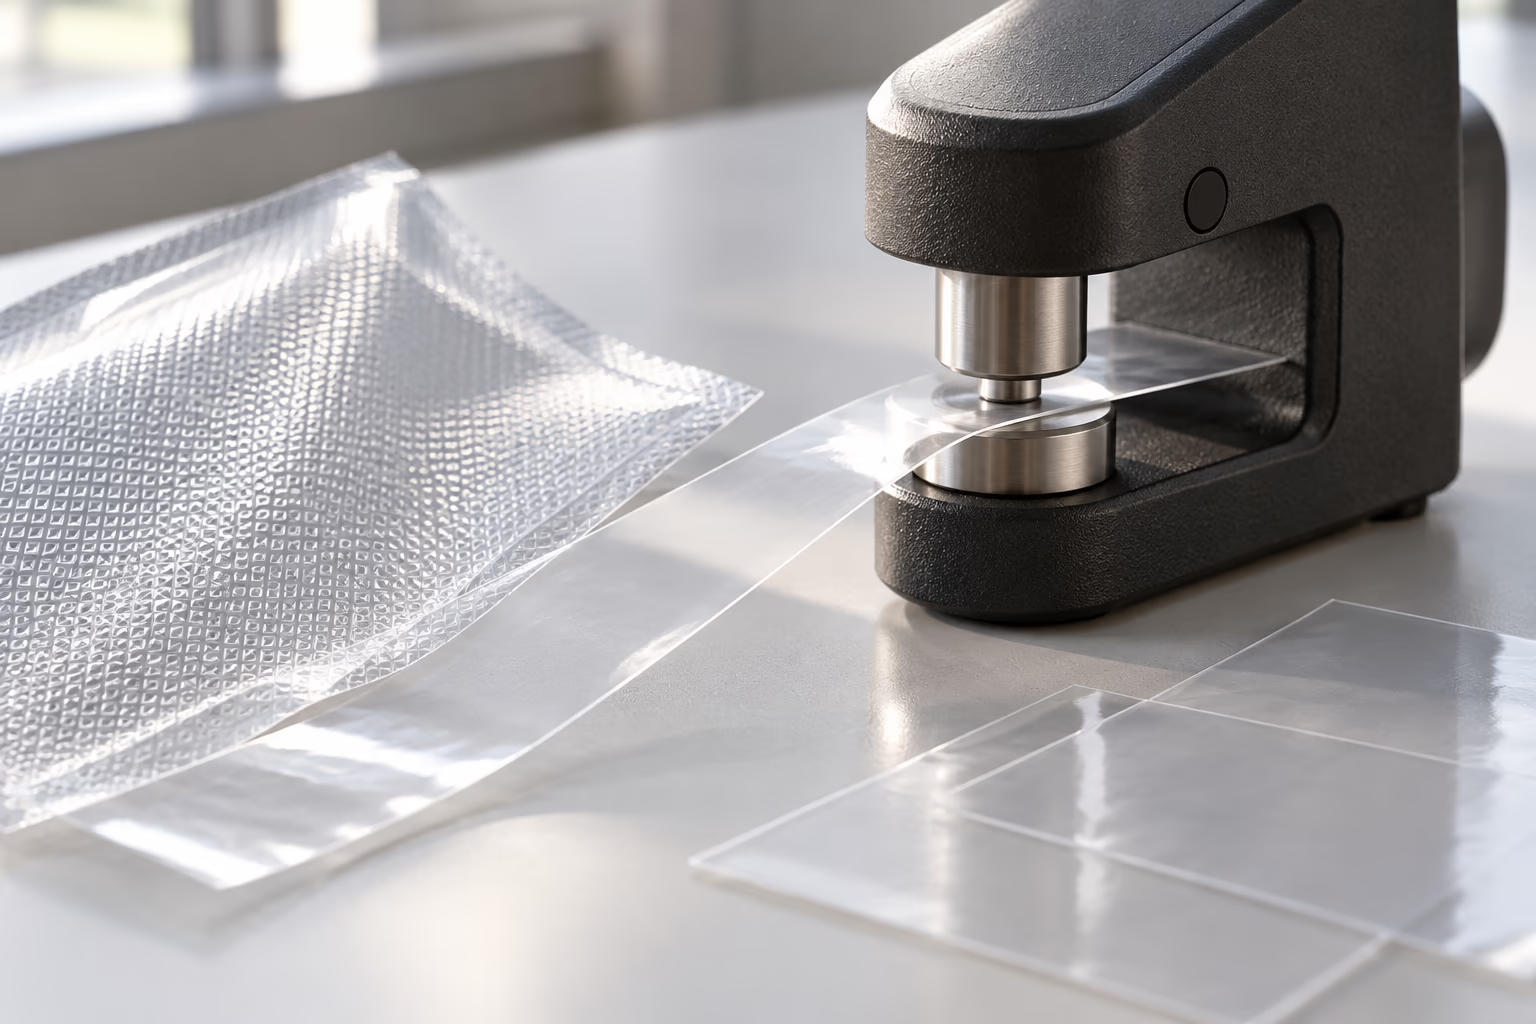
A micron is one micrometre, or one-thousandth of a millimetre. A mil is one-thousandth of an inch. The conversion is exact: 1 mil equals 25.4 micrometres. Therefore 100 micrometres is approximately 3.94 mil, and 4 mil is 101.6 micrometres.
Write the unit clearly in an RFQ or purchase specification. “Mil” does not mean millimetre. Preserve that distinction when comparing suppliers or translating an approved specification. A rounded retail description should not silently replace the tolerance on a technical drawing.
Define What Is Being Measured
Ask whether the quoted number describes one wall, the combined thickness of two walls, a nominal base film or a measurement that includes raised embossing. An embossed wall can have an uneven surface, so results depend on the measurement location and method.
A gauge reading on a folded or doubled pouch is not automatically a single-wall measurement. Averages can also conceal local thin areas. Agree the instrument, contact conditions, conditioning, sampling locations and reporting method with the supplier or test laboratory.
Record the nominal value and its permitted variation separately. Do not assume that every reputable supplier promises the same percentage tolerance. If two offers use different measurement definitions, resolve that difference before comparing their prices or apparent gauge.
Thickness and Puncture Resistance
For a fixed structure and comparable processing, changing gauge may change puncture behaviour. Across different films, resin grades, layer distribution, orientation, temperature and product shape can change the outcome. Total thickness does not describe all those variables.
For bone-in cuts or sharp products, evaluate the edge itself and consider an approved guard, pouch design or handling change. A thicker pouch is not a substitute for controlling an exposed sharp point. Test packing, chilling or freezing, movement and later handling with representative product shapes.
Sealing Settings Depend on the Complete Film
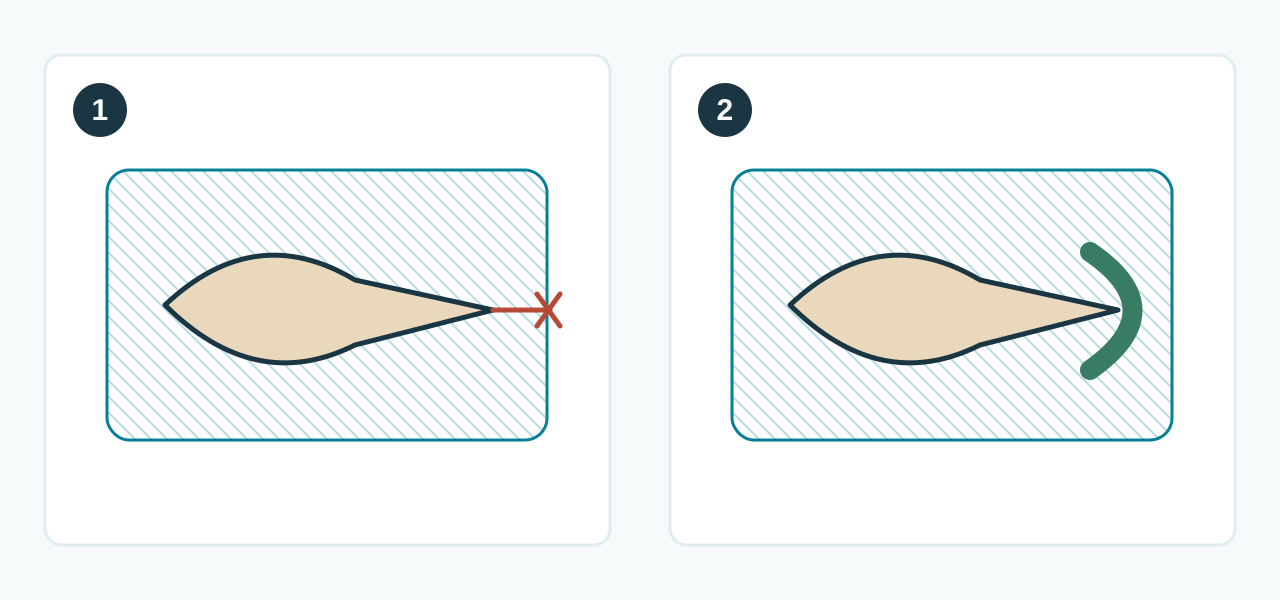
A different gauge or construction can require a different programme, but the appropriate adjustment comes from the material’s sealing window and the machine instructions. Do not automatically increase heater temperature whenever the quoted thickness increases.
Sealing energy, contact time, pressure and cooling interact with the sealant surface and the equipment. More heat can damage a film that was already adequately sealed. Less heat may leave a seam incompletely joined. Check repeated cycles as well as the first pack.
A consumer machine with limited controls must still be used within its approved consumable range. If a film cannot be sealed consistently within that range, choosing another pouch or machine is more reliable than repeatedly reheating a doubtful seam.
Use Gauge Bands as Sampling Options
A supplier may offer several nominal gauges for the same pouch family. Treat these as candidates to compare, not universal food categories. Firm dry goods, delicate produce, irregular proteins and heavy packs pose different risks even when their weight is similar.
Choose a small set of relevant samples with the supplier. Keep dimensions, product condition and process comparable, and record why each candidate passes or fails. A nominal 100-micrometre pouch does not automatically meet a bone-in or long-storage requirement.
For airflow, confirm embossed-bag compatibility separately. For oxygen barrier, request the actual structure and transmission data under comparable test conditions. Neither property can be established from the overall gauge alone.
Compare the Cost of Acceptable Packs
There is no universal price premium for increasing thickness. Film structure, dimensions, order quantity, embossing, printing, packing and current commercial terms all affect the offer. Request comparable quotations for defined specifications rather than applying a fixed percentage markup.
Include packing time, rejected samples, product loss, storage and transport requirements in the comparison. Do not invent an acceptable monthly failure count: define acceptance criteria for the actual commercial and food-safety process. Buying unnecessary gauge can also add cost and material without resolving the true defect.
Approve the Process and Incoming Lots
Before bulk ordering, test the real product on the intended machine at its expected workload. Examine film condition, full seam continuity, punctures, evacuation and the agreed leak or strength checks. A convenient small sample is a screening step, not proof of every possible handling condition.
Retain the approved pouch specification and samples where useful. On later lots, compare traceability, dimensions, gauge under the agreed method and packing performance. Investigate a change before accepting a batch simply because its label states the same thickness. See vacuum-bag quality control for the wider incoming-check process.