The pump removes air; the seam keeps the pack closed. They are separate jobs. A pouch can draw down neatly around the food and still fail later if its mouth was folded, contaminated or sealed with an unsuitable programme.
Heat sealing joins the pouch’s compatible inner surfaces under controlled contact and heat. Understanding that small area of film explains more about a failed pack than watching how tightly the bag first hugs the product.

What Actually Joins Together
Many vacuum pouches use a heat-sealable polyethylene-based inner layer. With the right combination of energy, contact pressure and time, the opposing inner surfaces join. The outer and barrier layers have different roles, and the complete film must tolerate the selected process.
This does not mean the entire pouch should melt, or that every film has the same temperature window. Seal-layer formulation, structure, thickness and surface condition affect what works. Two pouches with the same overall thickness may need different programmes.
The pouch materials guide explains why a film description such as PA/PE is only part of the specification. It does not give you a universal sealing temperature.
Impulse Heating and Constant Heat
An impulse system supplies energy to its heating element for a controlled part of the cycle. Constant-heat equipment maintains heated sealing surfaces. The controls, cooling sequence and suitable materials depend on the particular assembly.
Not every vacuum sealer uses the same heating ribbon, cover or bar arrangement. Some machines seal from one side, some from both, and some make more than one seam. A photograph of a closed lid cannot establish which system is inside it.
Likewise, the number on a control may mean sealing duration, a programme level or a temperature setpoint. Read the manual before interpreting it as degrees at the film interface. The heater temperature and the temperature where the two inner surfaces meet are different measurements.
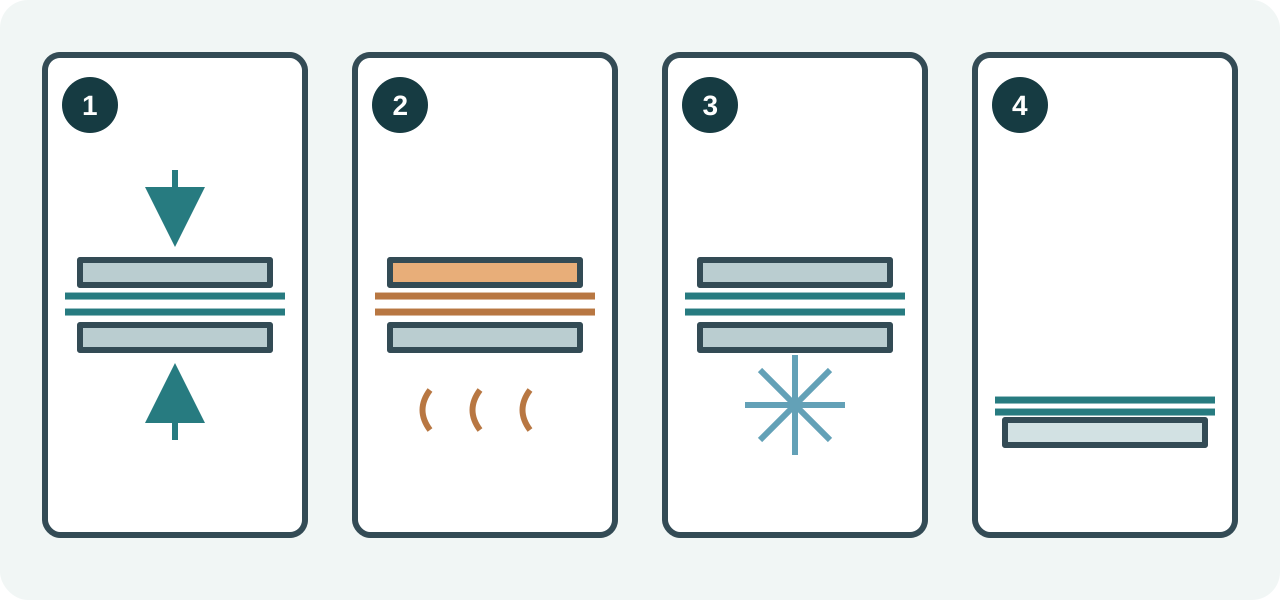
Heat, Contact and Time Work Together
Heat must reach the sealing surfaces, and the pouch must make even contact across the intended seam. A wrinkle or trapped food particle interrupts that contact. More heat does not reliably close the resulting channel.
Contact pressure also matters. Too little or uneven pressure can leave an incomplete area. Excessive pressure combined with excessive heat can distort or thin the film. These are reasons to check the process, not instructions to adjust an internal clamp mechanism yourself.
Changing film is a good point to review the starting programme. Begin with the equipment and pouch suppliers’ guidance. Change only the settings available to the operator, keep a record, and inspect cooled samples. Thicker film alone is not enough reason to increase every setting.
Why the Cooling Stage Matters
A freshly formed seam can behave differently while hot than after it has cooled. Hot-tack testing and cooled-seal strength testing address different conditions; ASTM F1921/F1921M describes the hot-seal subject.
Follow the machine’s completion signal and opening sequence. Do not force the lid open early or pull a heavy pouch by its new seam. Also observe any rest required before the next cycle. A machine recovery interval and a finished-seam handling interval solve different problems.
For a busy packing station, place a clear area beside the machine so the pack can be supported without stretching the hot seam. That is a small workflow change with a clear purpose: removing unnecessary load while the seam develops handling strength.
What the Finished Seam Can Tell You
An uninterrupted, evenly formed seam is a useful visual starting point. It is still only a starting point. Small channels and leaks can escape visual inspection, and a good-looking strip does not certify the package.
A fold through the strip points you back to pouch positioning. Film sticking or a repeated thin spot calls for checking the programme and the user-accessible sealing surface after cooling. A failure that appears only after a series of packs suggests reviewing the required rest pattern as well.
Keep the distinction between bar length and seam width. Bar length affects how much pouch mouth can be accommodated; seam width is the depth of the fused strip. There is no single minimum width that guarantees all vacuum pouches will remain closed. See the specifications guide for the dimensions to compare.
Cleaning without Damaging the Assembly
Before cleaning, disconnect power and allow hot parts to cool. Follow the model’s cleaning instructions for removable trays, cushions and protective surfaces. Do not assume that alcohol, abrasive pads or a scraper are suitable for every cover or adhesive.
A protective non-stick covering may be a wear item, but its material and replacement method are model-specific. Stop using damaged components and obtain the correct part and procedure. Replacing a heater wire or adjusting an internal assembly may require service.
Establish a Repeatable Programme
Use the actual pouch and product to confirm a programme, then record the film identity, setting, filling method and required pauses. Include the storage or downstream process the pack will encounter; a seam checked immediately at room temperature has not necessarily been assessed for every later condition.
When a fault returns, compare it with that record before changing the process. Our seal-failure guide follows the next checks in order, from the pouch mouth to damage elsewhere in the pack.