A vacuum-sealer pressure figure describes pressure at a stated measurement point. It does not by itself tell you how much oxygen remains in a filled pouch, how strong its seam is or how long food can be stored. To compare machines, first establish the pressure reference, units and test method, then compare the actual packing result.
Gauge Pressure and Absolute Pressure
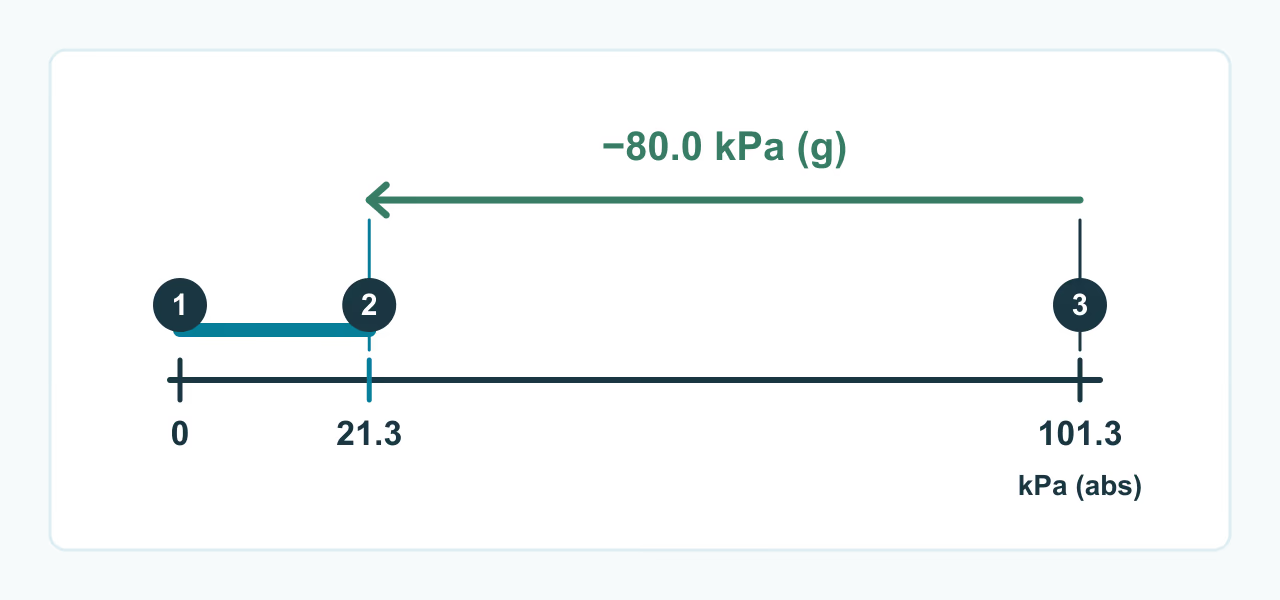
Absolute pressure is measured relative to a perfect vacuum. It is zero at that reference and is not negative in ordinary vacuum measurement. Gauge pressure is measured relative to the surrounding atmospheric pressure. A vacuum reading expressed as gauge pressure is negative because it is below that local atmosphere.
Use the relationship: absolute pressure = local atmospheric pressure + gauge pressure. With a stated atmosphere of 101.3 kPa, a reading of −80.0 kPa gauge corresponds to 21.3 kPa absolute. The same physical pressure is being described with two different reference points.
Local atmospheric pressure changes with altitude and weather. Standard atmosphere is a defined reference of 101.325 kPa, not a promise that every workshop has that pressure. At another local atmosphere, the same gauge reading corresponds to a different absolute pressure. Always ask whether a quoted positive number is absolute pressure, a pressure difference or an unsigned marketing description.
Converting kPa, mbar, mmHg and inHg
kPa and mbar are pressure units, not separate types of vacuum. Changing the unit does not change the pressure reference. A gauge value remains a gauge value after conversion; it does not become absolute pressure because it is written in mbar.
| Reference | kPa | mbar | mmHg | inHg |
|---|---|---|---|---|
| Unit ratio | 1 | 10 | 7.5006 | 0.2953 |
| Gauge example | −80.0 | −800 | −600 | −23.6 |
| Absolute example | 21.3 | 213 | 160 | 6.29 |
The two example rows describe the same condition only when the local atmosphere is 101.3 kPa. Rounding explains small differences. Do not add a minus sign to an absolute-pressure specification. If a supplier quotes a vacuum percentage, ask for its definition and reference rather than treating it as an oxygen-removal percentage.
Where Was the Pressure Measured?
A pump’s ultimate pressure may be measured with its inlet blocked under defined conditions. A reading in a suction channel or chamber belongs to that location. The filled pouch has its own flow restrictions, product geometry and changing volume. These measurements should not be presented as interchangeable.
An empty-bag test, a dry solid product and a liquid-rich portion are different tests. Cycle time, pouch texture, neck placement, gaskets and the chosen programme can affect the result. Ask whether the published figure is a pump rating, a cycle endpoint or a measured package result, and request the stated conditions.
The VATA35 and other VANTASE machines should be compared as specific models, with compatible pouches and representative products. A model’s listed maximum is not a guarantee that every filled bag reaches that condition.
External and Chamber Machines: Avoid Category Limits
Channel-type external sealers remove air through the pouch mouth while the product stays outside. Embossed passages help preserve the air path. Chamber machines lower pressure around the whole open pouch, seal it at reduced pressure, then admit air into the chamber.
These operating differences affect bag format, liquid handling, package geometry and workflow. They do not establish one universal maximum pressure for every external machine or prove that every chamber machine makes stronger seals. Avoid assigning fixed pressure bands to entire machine categories without model-specific evidence. Read the external and chamber comparison alongside the pressure specification.
Why −80 kPa Does Not Mean 80% Less Oxygen in Every Bag
Pressure and gas quantity are connected for a defined gas volume and temperature. A flexible pouch changes shape as air leaves, food traps pockets, and water vapour or other gases may contribute to the reading. The oxygen concentration of gas that remains is also different from the total quantity of oxygen present.
A simple pressure ratio under an idealised fixed-volume assumption cannot establish the oxygen content of every real food pouch. Later oxygen exposure also depends on film permeation, leaks and storage conditions. If residual oxygen is an acceptance criterion, use a suitable package test with a defined sampling method rather than calculating it from the pump rating.
Is Deeper Vacuum Always Better?
Greater air removal may help some quality goals, but the product and process determine the useful setting. Soft foods can deform as atmospheric pressure presses film against them. Sharp edges can load the pouch locally. Liquid can boil during a low-pressure cycle when conditions reach its temperature-dependent boiling point; this is different from saying all sealed food slowly dries because the displayed vacuum is high.
Seam quality needs compatible film, clean contact surfaces, suitable heat and cooling. Food safety needs its own controls. Deeper vacuum does not sterilise food or provide a universal shelf-life increase. See food shelf life and sous vide packing for the related application limits.
How to Compare Two Specifications Fairly
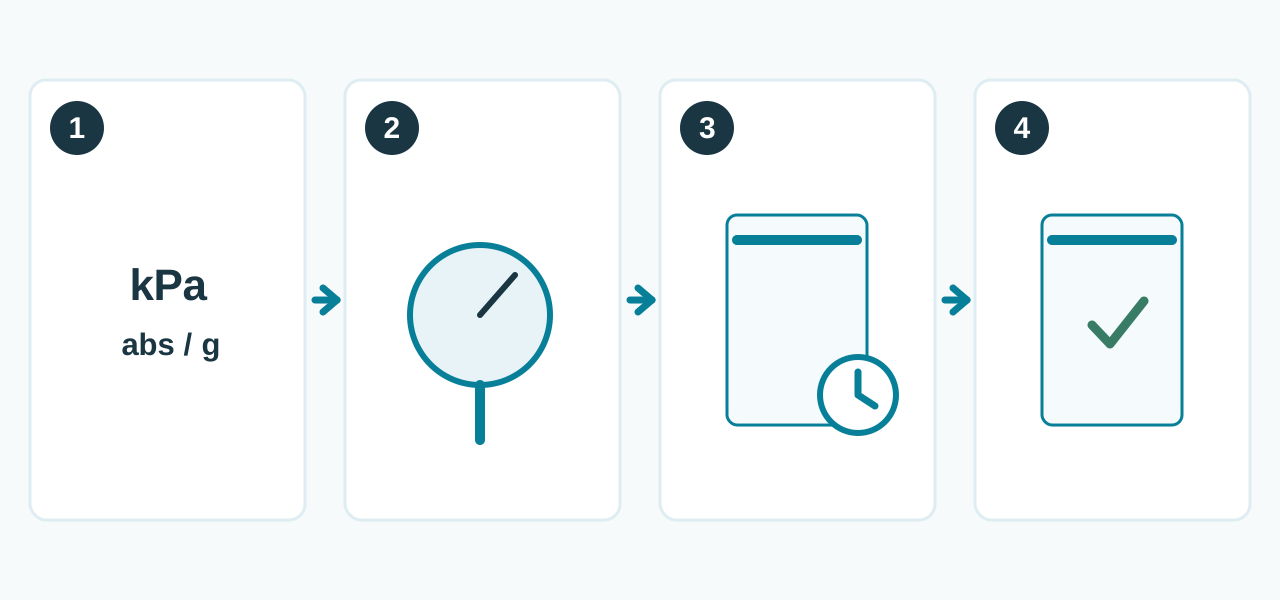
Request a record of local atmosphere, measurement point, instrument range and calibration, product temperature, pouch format and cycle endpoint. If readings are logged over time, compare the same defined stage rather than a brief peak on one machine with a different endpoint on another. There is no universal peak-to-settled correction that applies to every model.
For your own measurements, use only a manufacturer-approved test connection and a suitable instrument with a documented method. An improvised hole in a bag or modified food-contact hose can create leaks and change the result. Installation or internal work should be handled by qualified personnel. Leybold’s explanation of direct pressure measurement shows why instrument design and atmospheric reference matter.
Combine pressure records with cycle time, repeatability, seam condition, appropriate leak testing, product deformation and service needs. A representative trial answers a purchasing question more directly than an isolated maximum number. Contact VANTASE with the product, pouch and required test conditions for a model comparison.